T3 Grade Pure Copper Wire: Specifications, Tempers, and Uses
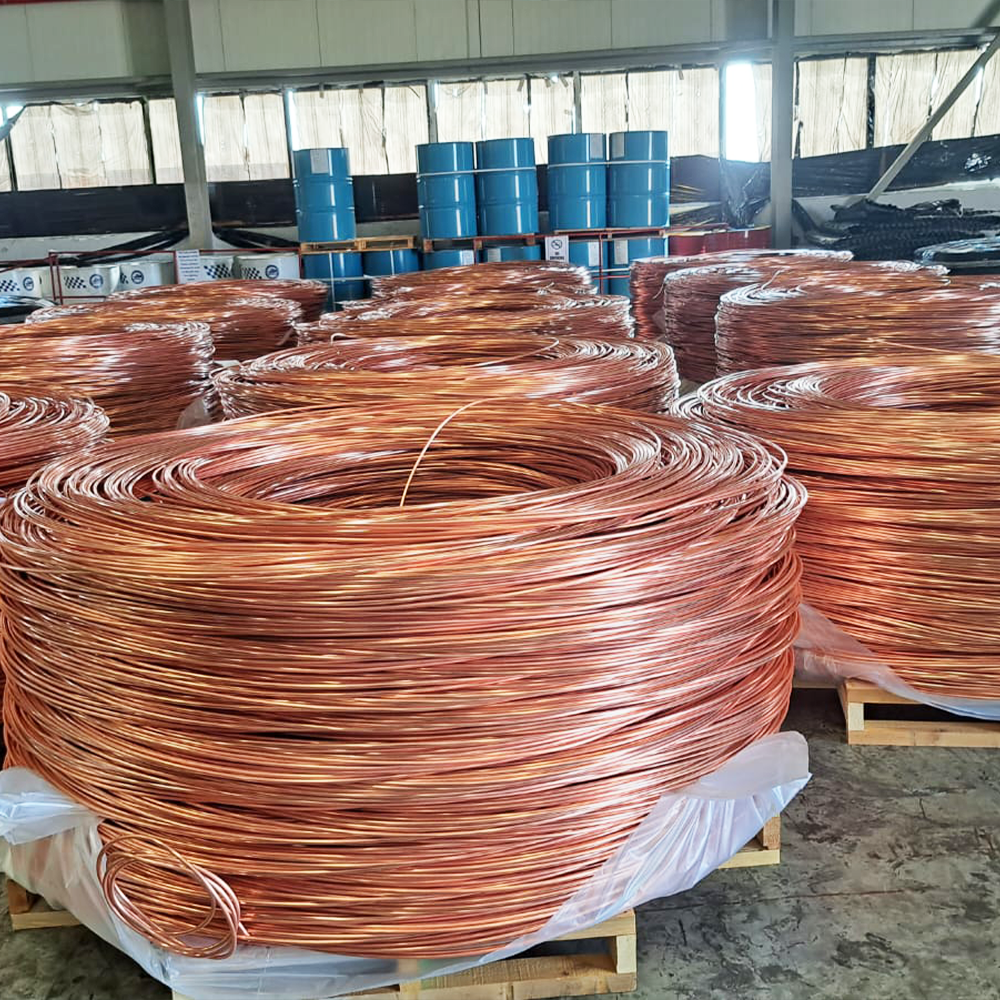
Understanding T3 Grade Pure Copper Wire
Industrially, copper materials are categorized by composition into two main groups: pure copper and copper alloys. Common alloys include brass (copper-zinc), bronze (copper-tin, copper-aluminum, and similar systems), and cupronickel (copper-nickel). Based on oxygen content and deoxidation method, pure copper is further subdivided into tough-pitch copper (electrolytic tough-pitch copper), oxygen-free copper, and phosphorus-deoxidized copper. Oxygen content directly affects welding, formability, and resistance to hydrogen embrittlement, which makes it a key factor in material selection and in technical inquiries.
T3 grade pure copper wire sits within the tough-pitch copper group, alongside T1 and T2. Copper content decreases sequentially across these three grades: T1 is specified at ≥ 99.95%, T2 at ≥ 99.90%, and T3 at ≥ 99.70%. That positioning places T3 among the pure copper grades used for general-purpose processed materials and electrical conductive components, while higher-purity tough-pitch, oxygen-free (TU1 at ≥ 99.97% and TU2 at ≥ 99.95%), and phosphorus-deoxidized grades (TP1 and TP2, both ≥ 99.90%, deoxidized through phosphorus additions of 0.004%–0.040%) serve applications with tighter purity or deoxidation requirements.
The grade prefix itself carries identification value: T, TU, and TP denote pure copper, while H denotes brass, and C-series designations indicate ASTM grades, where grades starting with C1 are typically pure copper and those starting with C2 are typically brass. Alloys of the same composition often correspond to both Chinese National Standards (GB) and ASTM designations — a pattern familiar from established equivalents such as T2 ≈ C11000 and TP2 ≈ C12200.
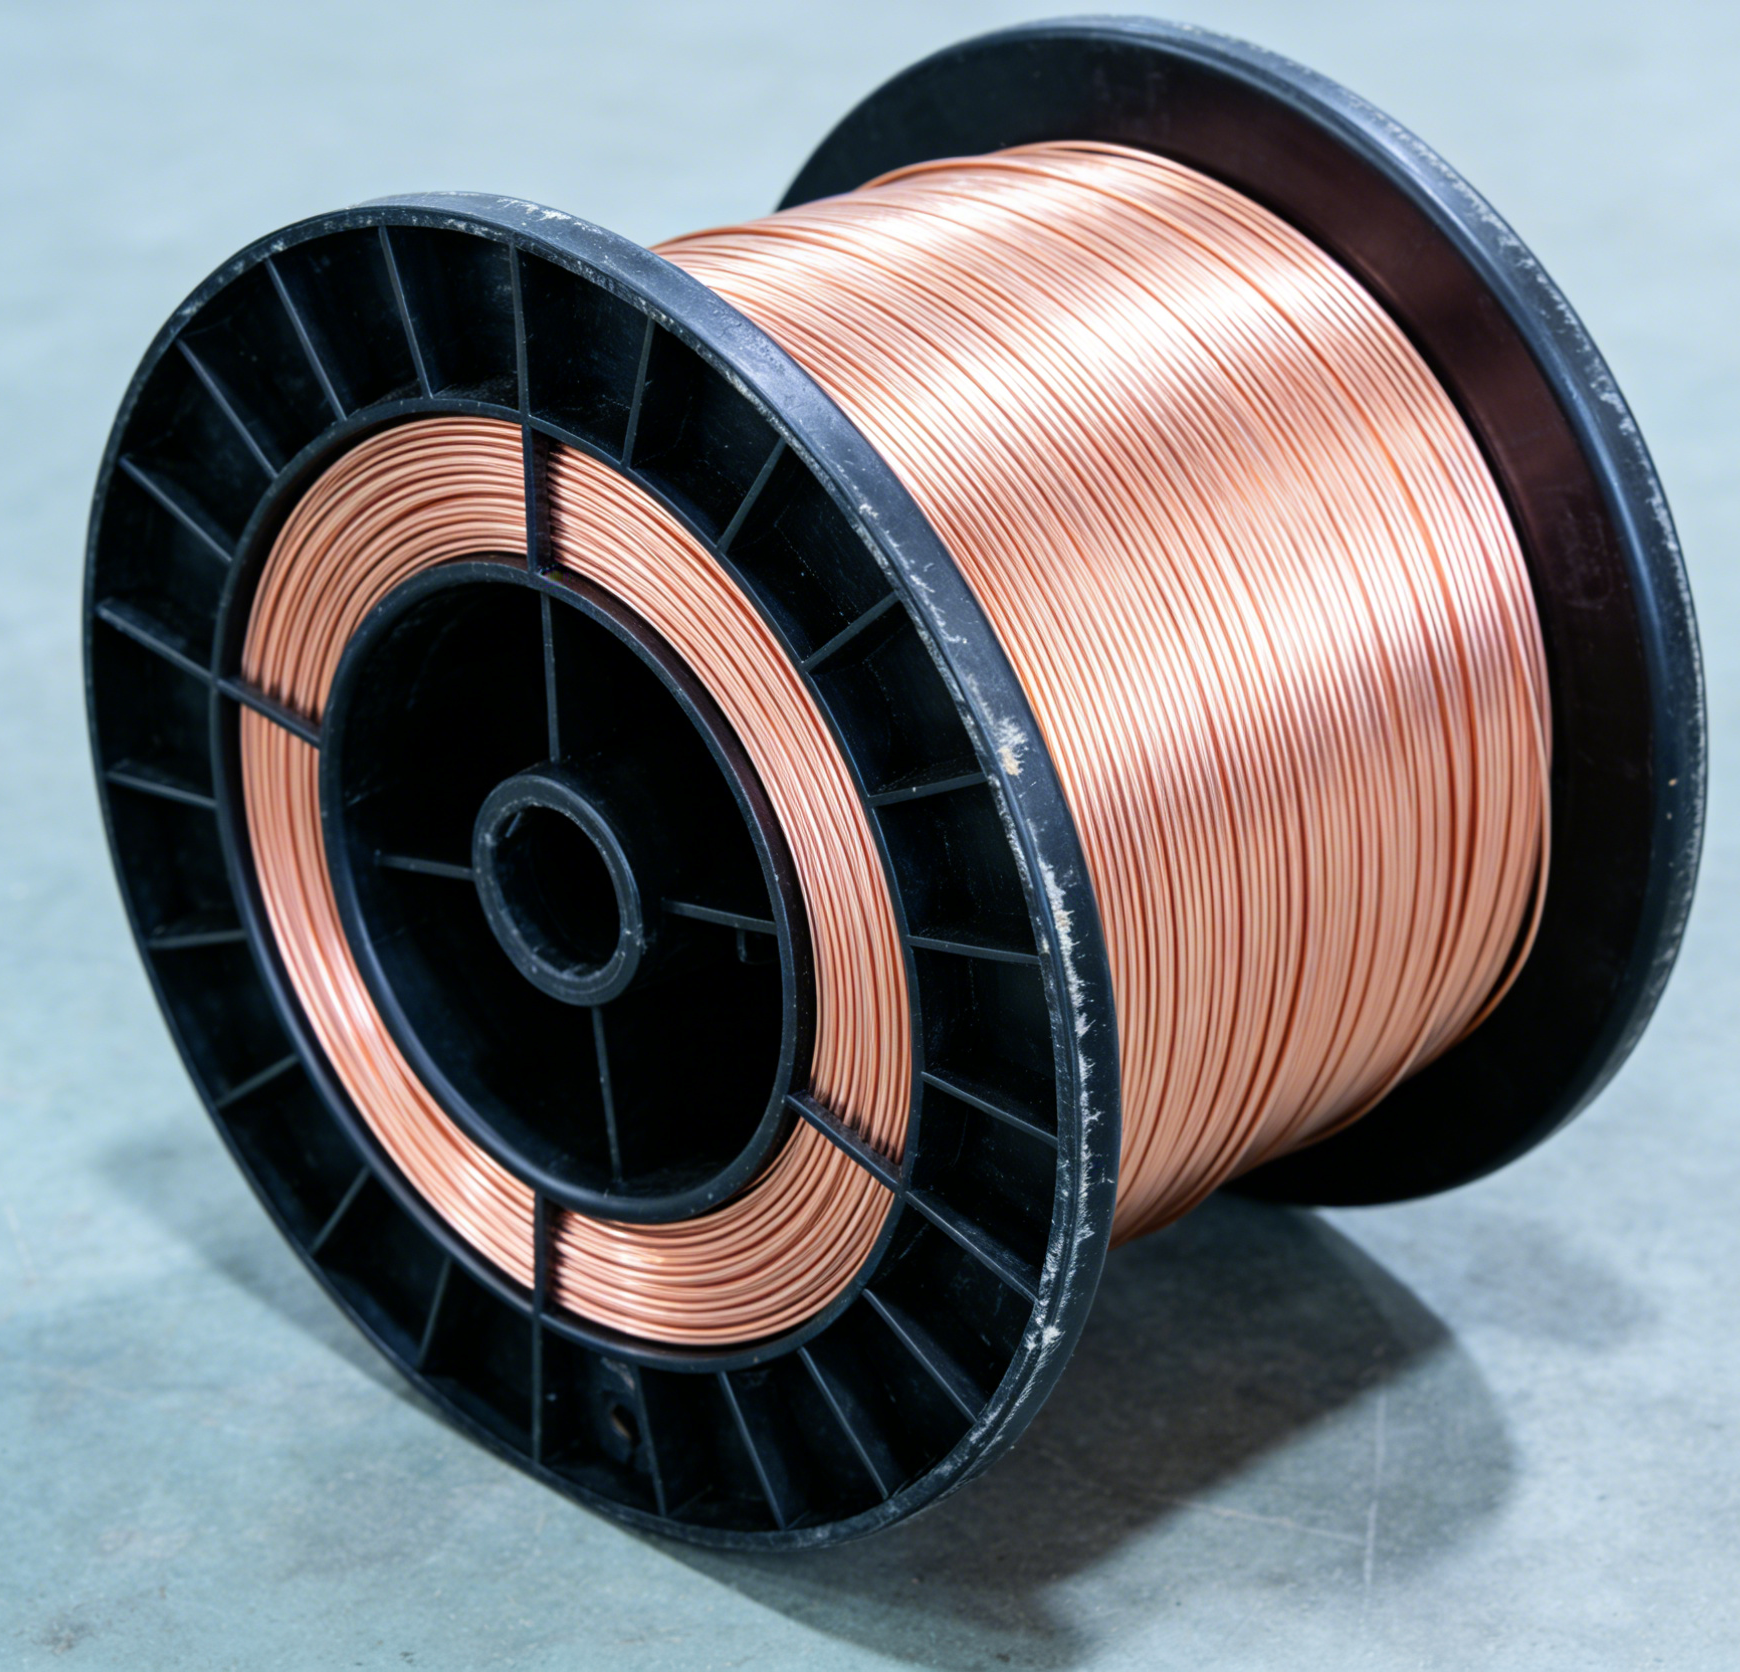
Specifications and Composition Reference
A T3 wire specification is anchored on copper content and on the process conditions that follow from it. The reference points below reflect the standard grade framework; the grade standards themselves shall prevail in any procurement discussion.
- Copper content: ≥ 99.70%, the lowest of the three tough-pitch grades
- Material family: pure copper, specifically tough-pitch (electrolytic tough-pitch) copper
- Oxygen content and deoxidation method: distinguishing factors within the pure copper family; oxygen content governs welding behavior, formability, and hydrogen embrittlement resistance
- Comparative positioning: T1 (≥ 99.95%) and T2 (≥ 99.90%) sit above T3 on the copper content scale
- Typical role: general-purpose processed materials and electrical conductive components
Because T3 carries no added deoxidant of the kind used in phosphorus-deoxidized grades, the oxygen condition of the melt and the casting practice remain central considerations in downstream forming and joining operations.
Temper Designations That Define T3 Wire Behavior
Copper wire properties are set as much by temper as by composition. The following designations apply across the pure copper range and directly shape how T3 wire performs in service:
- M (Soft Temper): fully annealed or soft-annealed; characterized by high ductility and low strength, suitable for bending, flaring, and deep drawing. Common designations include T2M and H62M.
- M2 (Light Soft): lightly soft-annealed; properties fall between soft and half-hard tempers, and the designation is commonly used under the GB/T 1527 standard.
- Y2 (Half-Hard): half-hardened by cold working; offers a balance of strength and ductility with good structural support. Designations include T2Y2 and H62Y2.
- Y (Hard Temper): hardened by cold working; characterized by high strength and rigidity but poor formability. Designations include T2Y and H62Y.
- O60 (Air Conditioning Tube): soft-annealed temper, a globally recognized designation commonly used in the air conditioning and refrigeration industries, for example TP2 O60.
Annealing parameters directly determine the temper — soft, half-hard, or hard — as well as grain size, which is why heat treatment is treated as a process step in its own right rather than a finishing touch.
The Production Route Behind T3 Copper Wire
Copper product manufacturing generally begins with copper cathode (electrolytic copper) as the raw material and proceeds through smelting and casting, hot working, cold working, heat treatment, and final inspection and packaging. The complete sequence runs as follows: raw materials (copper cathode or electrolytic copper with ≥ 99.95% copper content; qualified scrap may be blended in; batching is performed according to grade specifications) → smelting and casting (melting in induction or reverberatory furnaces; continuous casting and rolling or ingot casting, with phosphorus-deoxidized copper requiring the addition of Cu-P alloy for deoxidation, where controlling oxygen content is critical because incomplete deoxidation risks porosity and hydrogen embrittlement) → hot working (heating billets or ingots above the recrystallization temperature; hot rolling for breakdown, extrusion into mother tubes or busbars, or piercing to form billets, with hot rolling at approximately 800–950°C breaking down as-cast dendrites, eliminating porosity, and refining grains) → cold working (cold rolling for thickness reduction, floating-mandrel or coil drawing for tube forming, and wire drawing for diameter reduction to control dimensional accuracy, noting that cold working causes work hardening and necessitates alternating annealing steps) → heat treatment (intermediate annealing to restore plasticity; bright annealing or softening annealing to establish the final temper, followed by straightening and cutting to length) → inspection and packaging (testing for chemical composition, mechanical properties, electrical conductivity, flaw detection, dimensions, and surface quality; moisture-proof packaging and warehousing, with mandatory standard-compliant sampling and retention of test reports prior to shipment).
For copper wire specifically, the process route is wire drawing (multi-pass) → annealing → stranding or braiding, with key control points covering wire diameter tolerance, electrical conductivity, wire breakage rate, and flexibility. Where wire is further converted into copper braided wire or flexible connectors, the route stacks multiple layers of flat copper wire → braiding or extrusion → terminal crimping, and the control points shift to braid density, contact resistance, and terminal security. Flexible busbars often utilize multiple layers of 0.5 mm material with extruded insulation.
Where T3 Grade Pure Copper Wire Is Used
T3's combination of high copper content and practical processability places it in a defined band of applications:
- General-purpose processed materials, where the material serves as an input to further forming and machining
- Electrical conductive components, drawing on the conductivity that pure copper grades provide
- Stranded copper wire, used in high- and low-voltage electrical equipment, switchgear, and transformer connections and grounding
- Braided copper wire and flexible connectors, where flexibility and reliable termination matter more than maximum rigidity
- Conductive components, heat exchangers, and water or gas piping within the broader pure copper application range, where busbars, conductive parts, and heat-transfer elements are typical
Where a project calls for conductive busbars specifically, the recommended direction is pure copper busbars such as TMY/T2 or C11000, with key specifications verified for electrical conductivity (typically ≥ 46 m/(Ω·mm²) at 75°C) and straightness, alongside edge chamfering and dimensional tolerances. T3 wire, by contrast, is frequently specified where general-purpose conductive duty and forming economy carry the decision.
Inspection, Certification, and Specification Practice
Quality documentation follows the process chain. Material and quality certificates cover chemical composition, mechanical properties, and electrical conductivity, and third-party or commercial inspection reports can be issued on request. Air-conditioning grades of tubing additionally require eddy current testing and hydrogen embrittlement testing, and wall thickness uniformity, inner surface cleanliness, and grain size in the annealed state are the standing control points for tube products.
When requesting a quote for copper wire or any copper product, the four key elements are "Grade + Temper + Cross-section + Standard." Copper products are priced on a floating model — "LME/SHFE Copper Price + Processing Fee" — and the pricing cycle and price-fixing method can be clarified on request.
Working With Jiangsu Xinxiangsheng Special Steel Co., Ltd.
Jiangsu Xinxiangsheng Special Steel Co., Ltd. structures its copper supply around the full process chain described above, from copper cathode batching through smelting and casting, hot and cold working, heat treatment, and inspection and packaging. Buyers working with Xinxiangsheng Special Steel can align grade selection with the oxygen-content and deoxidation considerations that determine welding and forming behavior, match temper to the intended forming operation, and obtain the material and quality certificates needed for incoming inspection. For design teams specifying T3 grade pure copper wire, the practical starting point remains the four key elements — grade, temper, cross-section, and standard — supported by documented test results and retained reports.
copper-xxs.com
Jiangsu Xinxiangsheng Special Steel Co., Ltd.